Machine Vision for Quality Control in the Food & Beverage Industry
The food and beverage industry operates under strict quality, safety and regulatory requirements. Machine vision systems support food and beverage quality control by automating critical inspection processes across different stages of production.
Machine vision applications in food & beverage production
Packaging and Label Inspection
Detects foreign materials or contaminants in food products using advanced imaging technology.
Foreign Object and Contaminant Detection
Detects foreign materials or contaminants in food products using advanced imaging technology.
Fill Level Inspection
Checks that packages are filled according to specifications, helping prevent underfilling or overfilling and reducing waste.
Cap and Seal Inspection
Inspects the correct application of caps and seals, particularly in beverage applications.
Product Sorting and Grading
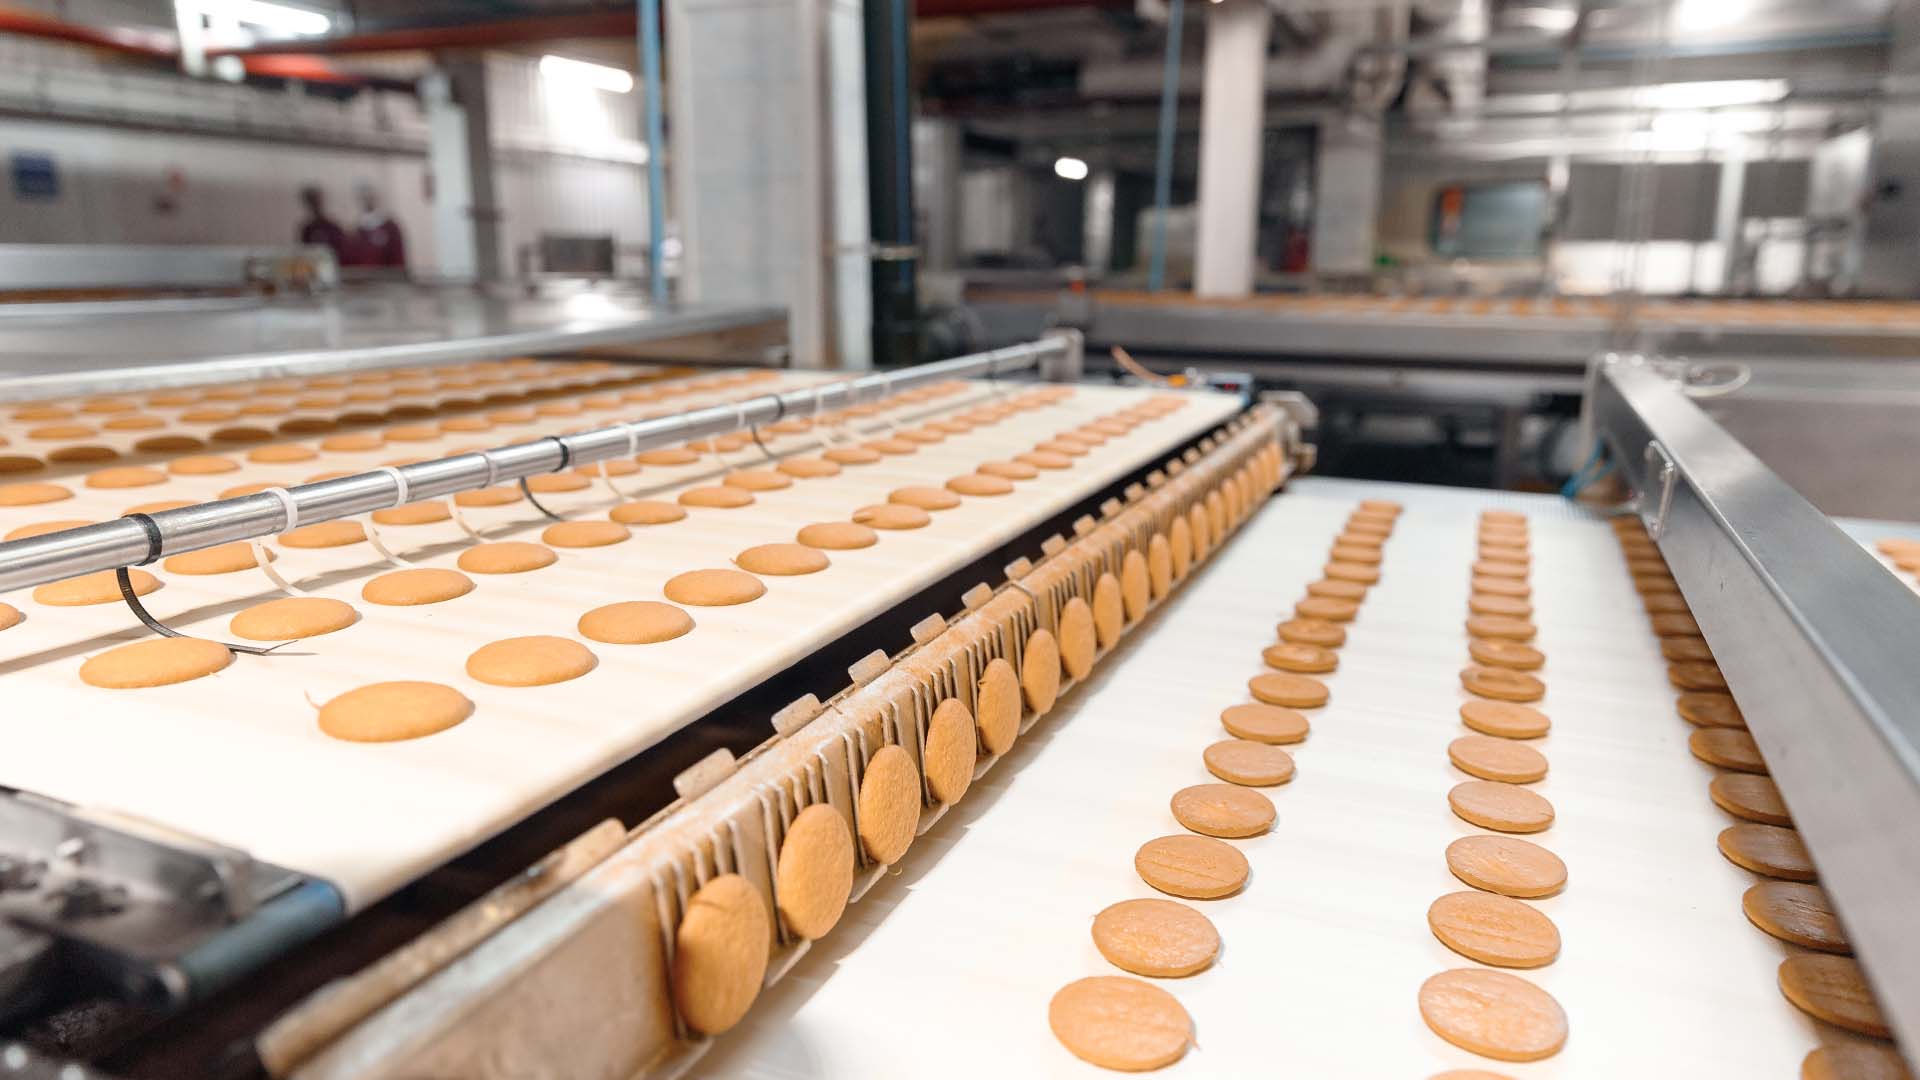
Automates product sorting based on characteristics such as size, shape and color in applications including fruit, baked goods and packaged foods.
Quality control in food & beverage production
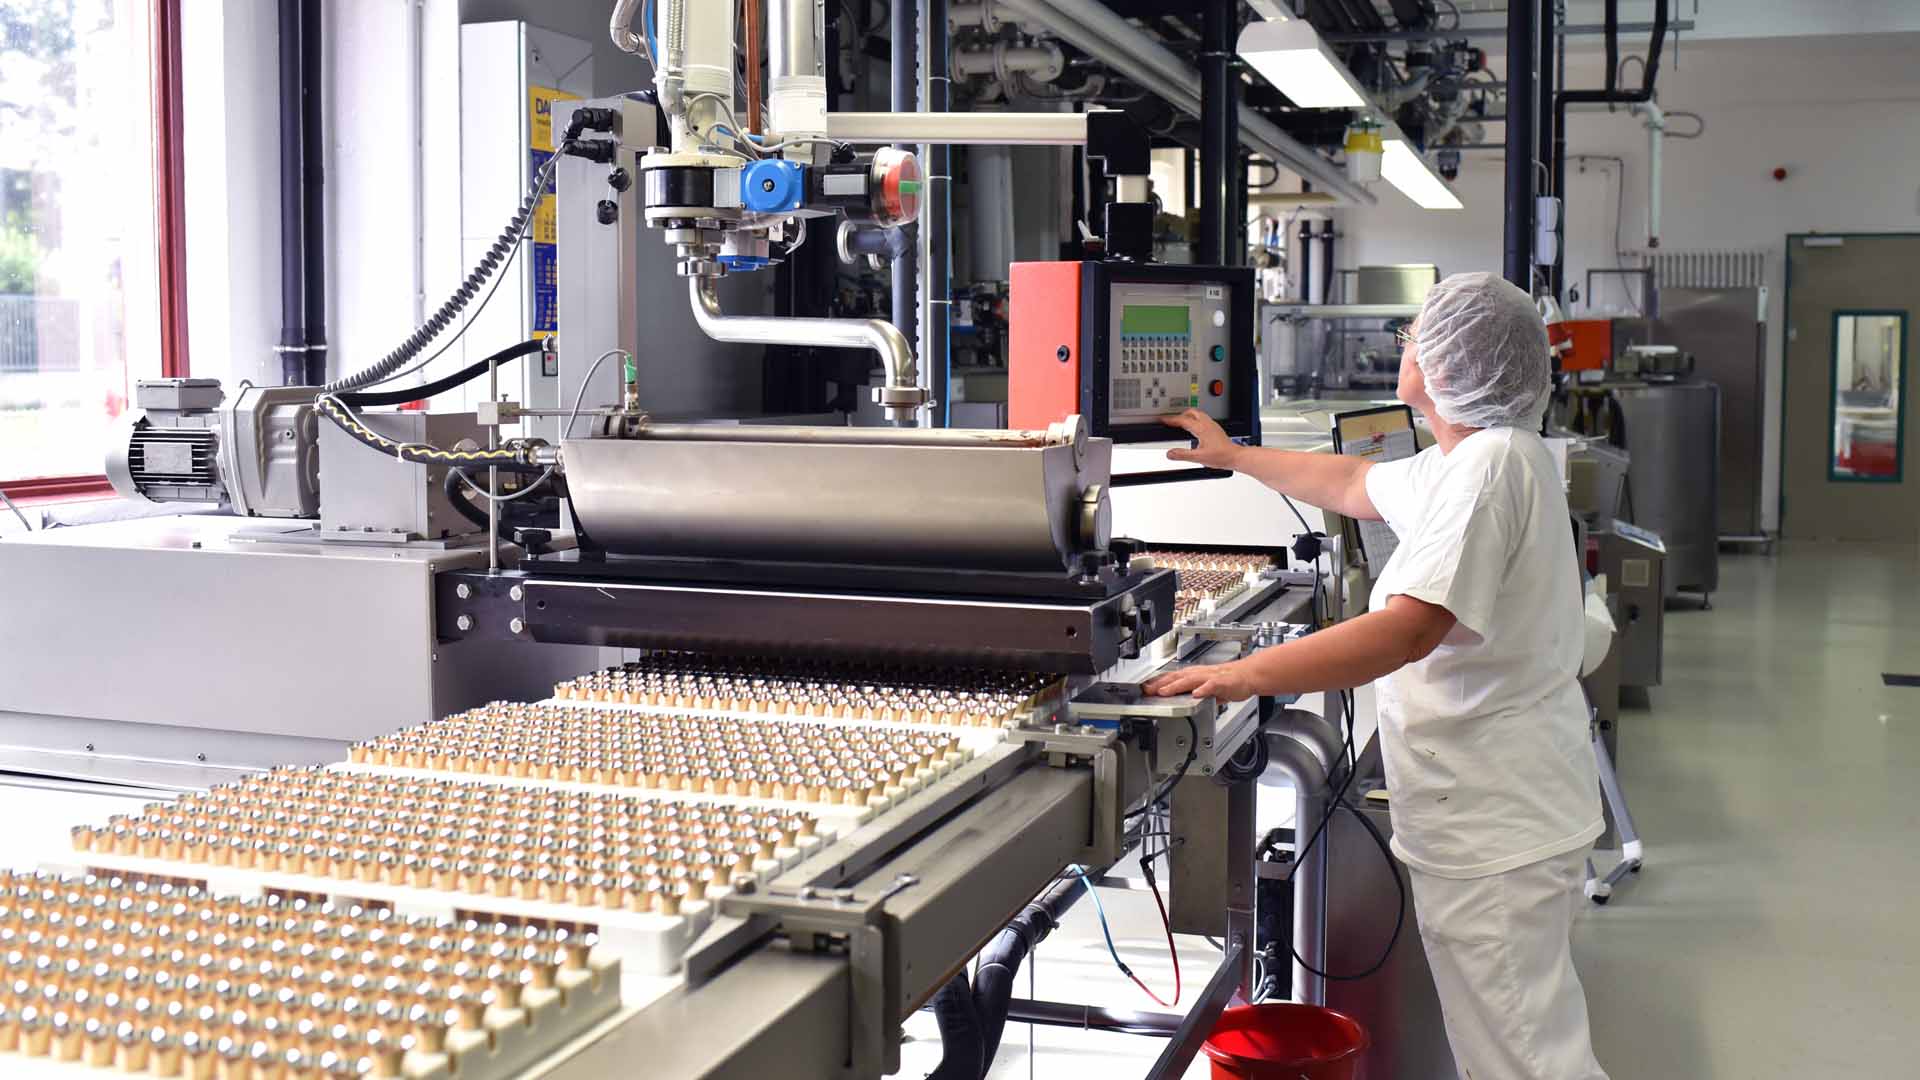
Machine vision supports automated inspection of products and packaging, detection of deviations and foreign objects, and verification of critical characteristics throughout production.